APPLICATIONS
What the AM-X makes
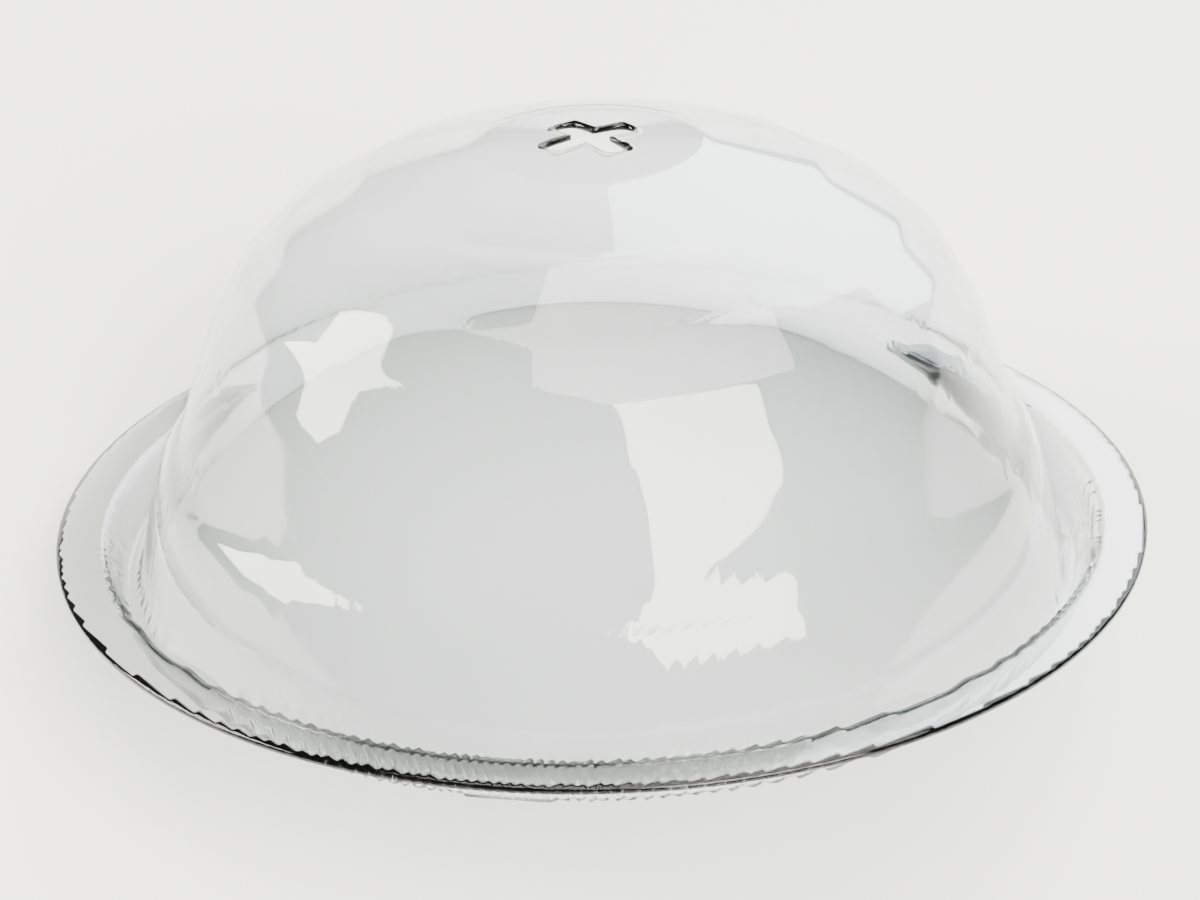
Dome lid for cold cups
Beverages, QSR
PET · 0.3 mm · 98 × 98 mm · 35 mm deep
20 per index (4 × 5)
| Model | Parts per hour |
|---|
| Eco | 14,800 |
|---|
| Mid | 17,880 |
|---|
| Pro | 27,310 |
|---|
clear PET, formed over a male plug
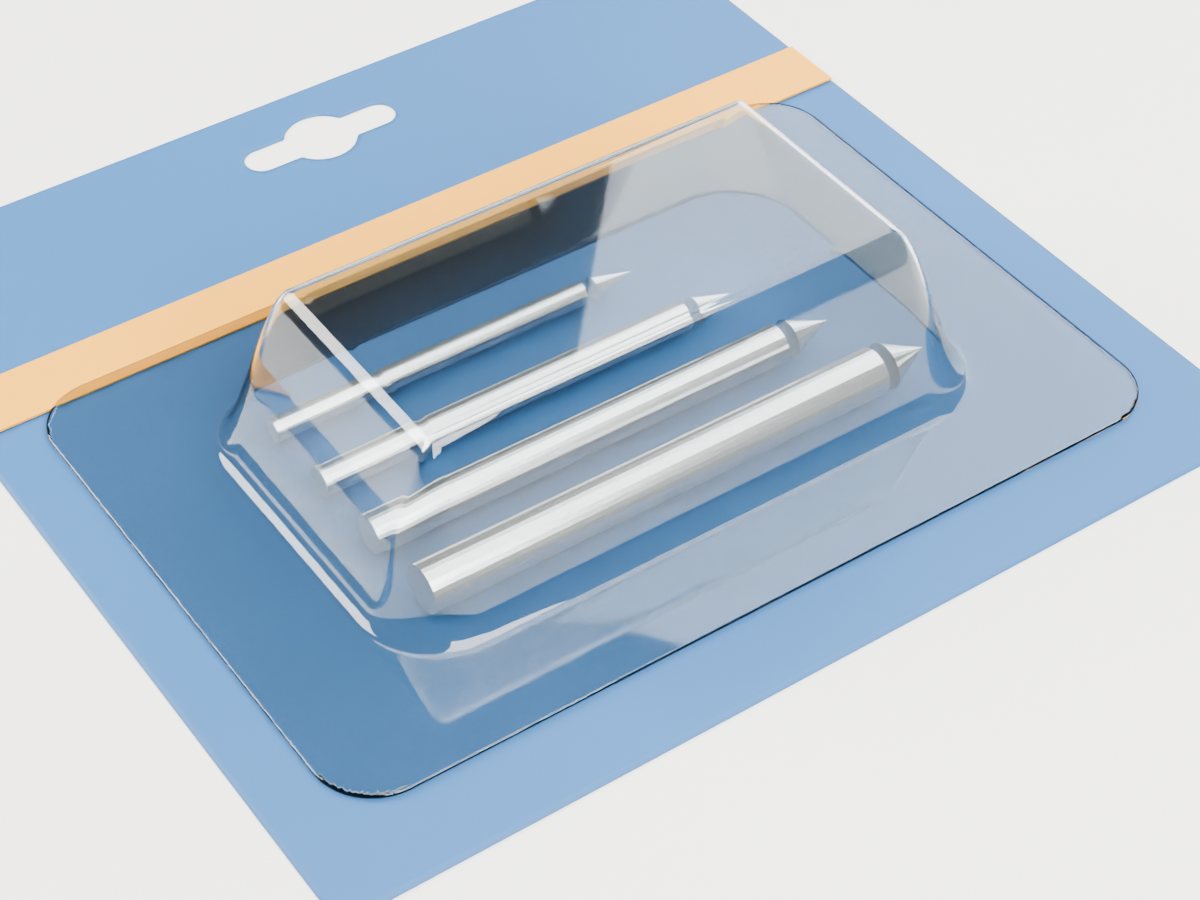
Hanging retail blister
Hardware, toys
PVC · 0.4 mm · 150 × 100 mm · 30 mm deep
15 per index (3 × 5)
| Model | Parts per hour |
|---|
| Eco | 10,820 |
|---|
| Mid | 13,100 |
|---|
| Pro | 19,950 |
|---|
clear PVC, sealed to a card
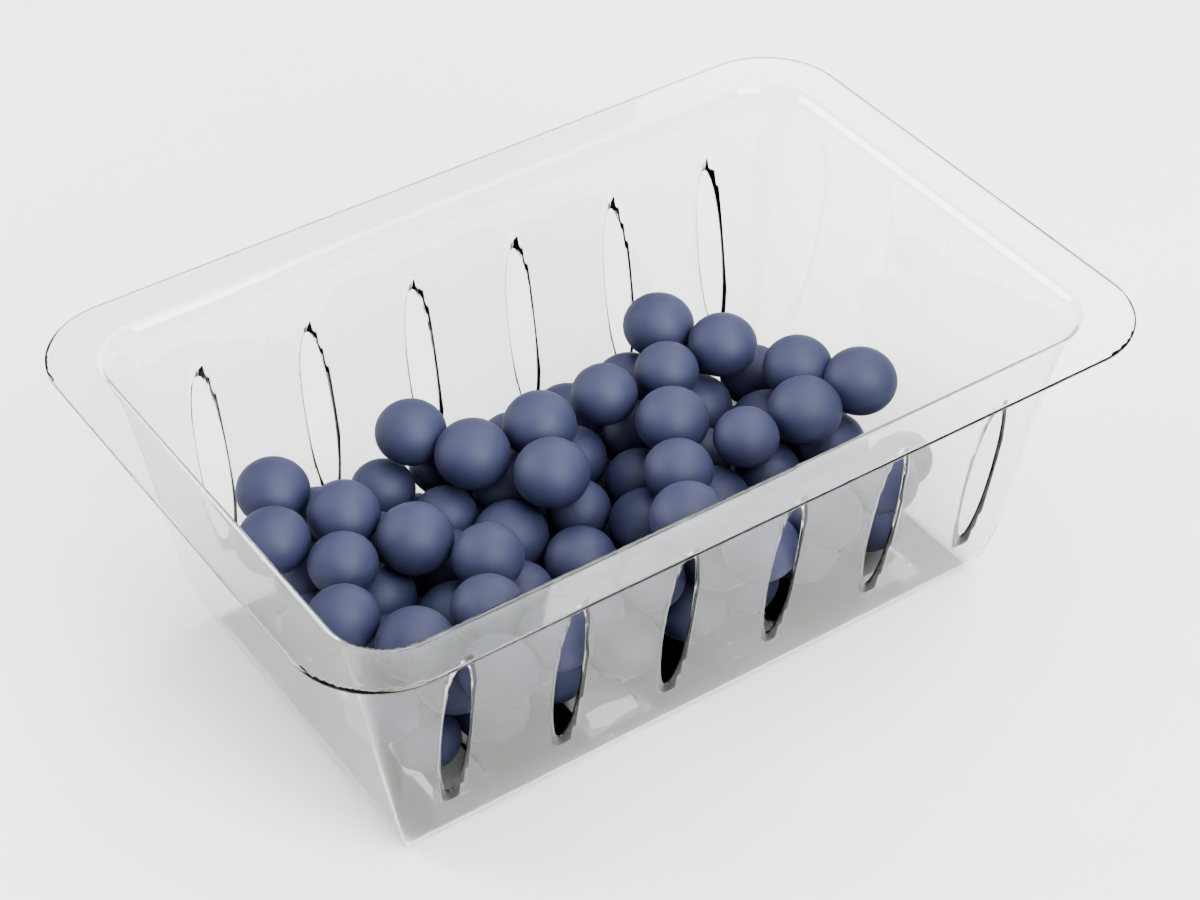
Berry punnet
Fresh produce
PET · 0.35 mm · 150 × 100 mm · 55 mm deep
12 per index (4 × 3)
| Model | Parts per hour |
|---|
| Eco | 8,610 |
|---|
| Mid | 10,430 |
|---|
| Pro | 15,870 |
|---|
clear PET, vented
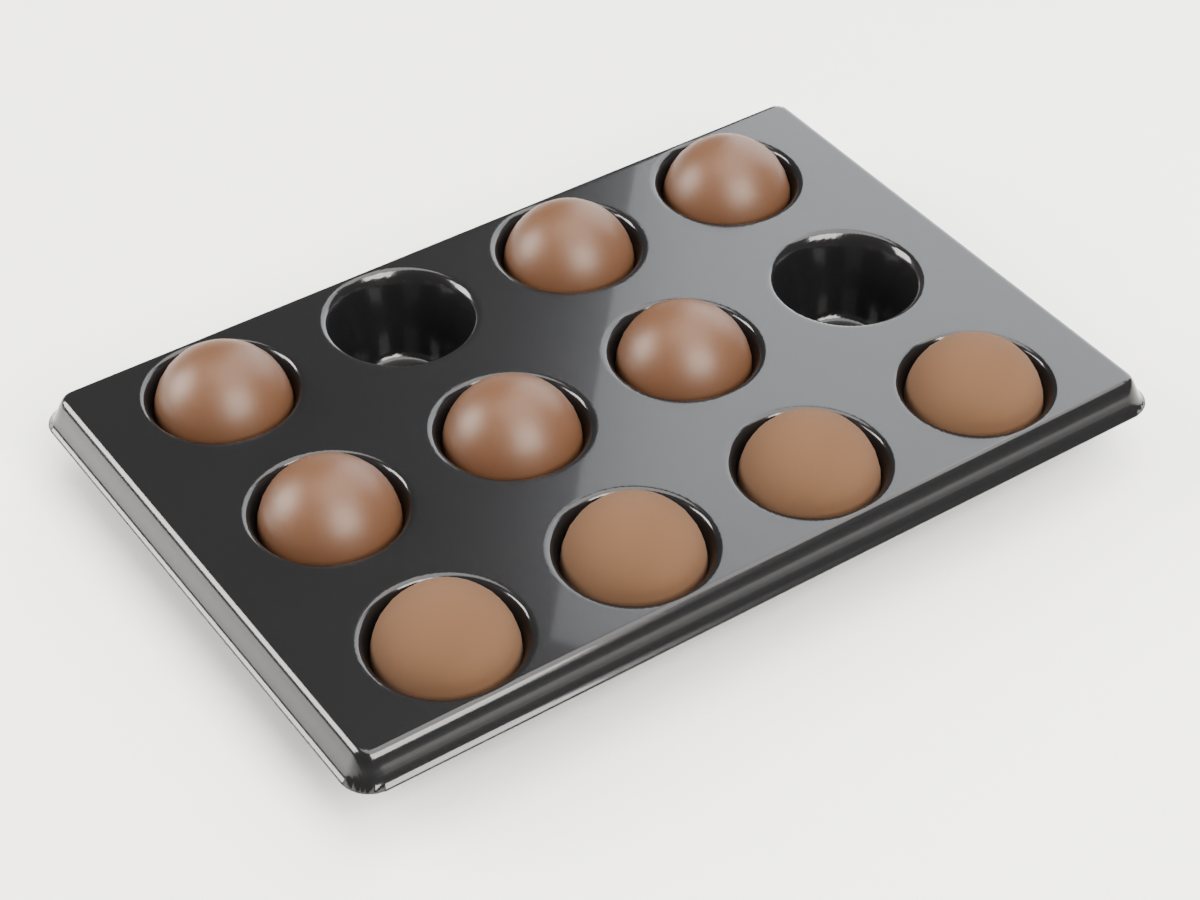
Chocolate box insert
Confectionery
HIPS · 0.3 mm · 180 × 120 mm · 18 mm deep
9 per index (3 × 3)
| Model | Parts per hour |
|---|
| Eco | 6,960 |
|---|
| Mid | 8,370 |
|---|
| Pro | 12,860 |
|---|
black HIPS, 12 pockets
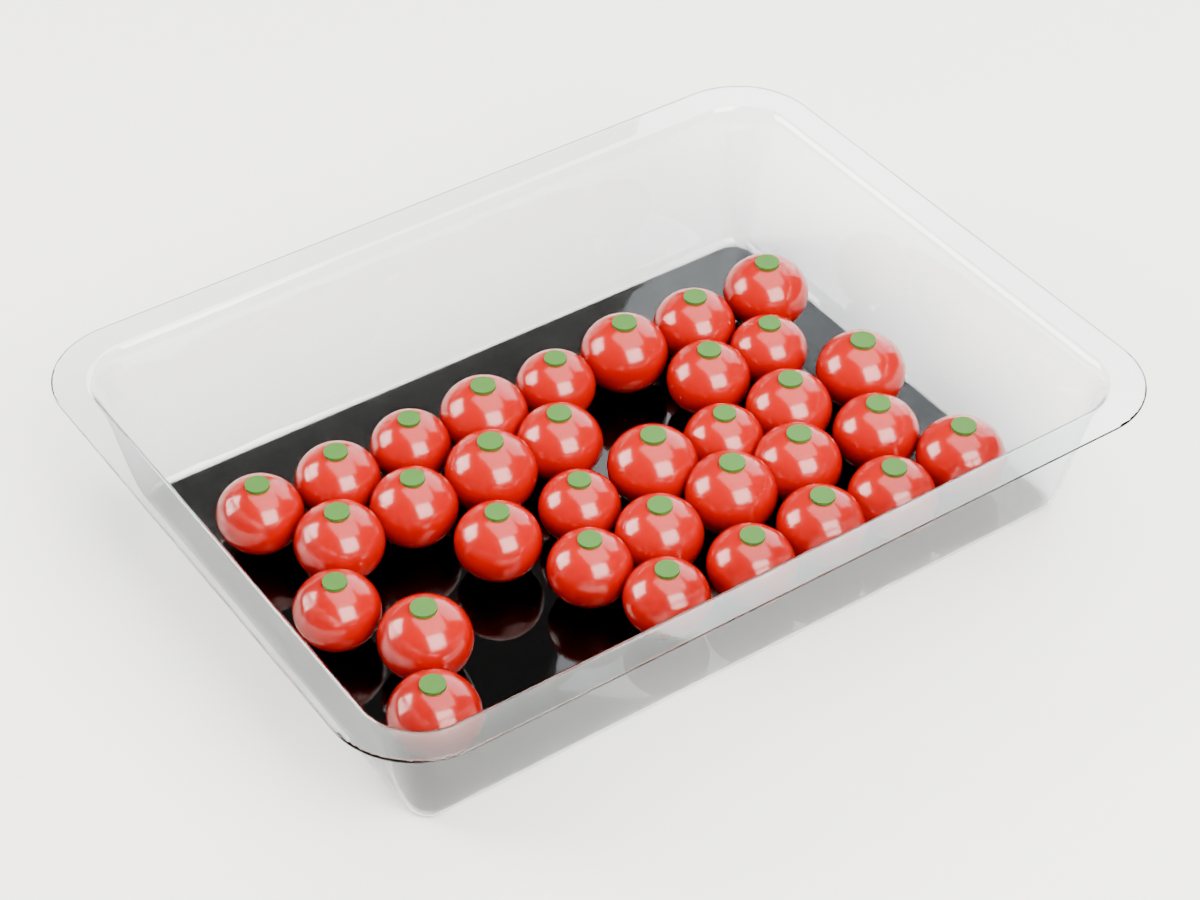
Fresh-cut vegetable tray
Fresh produce
PET · 0.5 mm · 230 × 175 mm · 40 mm deep
6 per index (2 × 3)
| Model | Parts per hour |
|---|
| Eco | 4,320 |
|---|
| Mid | 5,230 |
|---|
| Pro | 7,960 |
|---|
clear PET
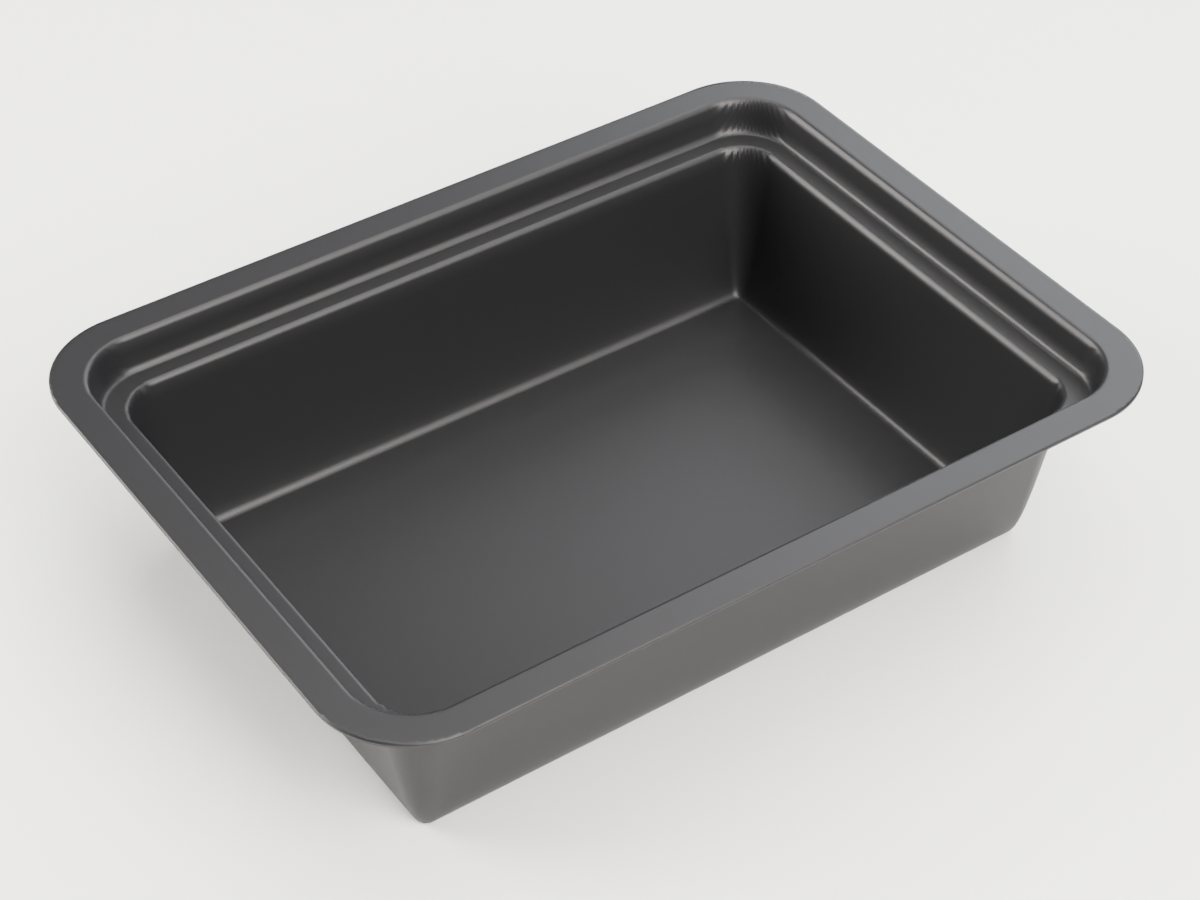
Ready-meal tray
Food service
PP · 0.8 mm · 190 × 140 mm · 45 mm deep
6 per index (2 × 3)
| Model | Parts per hour |
|---|
| Eco | PP needs heat from both sides |
|---|
| Mid | 3,840 |
|---|
| Pro | 5,220 |
|---|
black PP, microwave safe
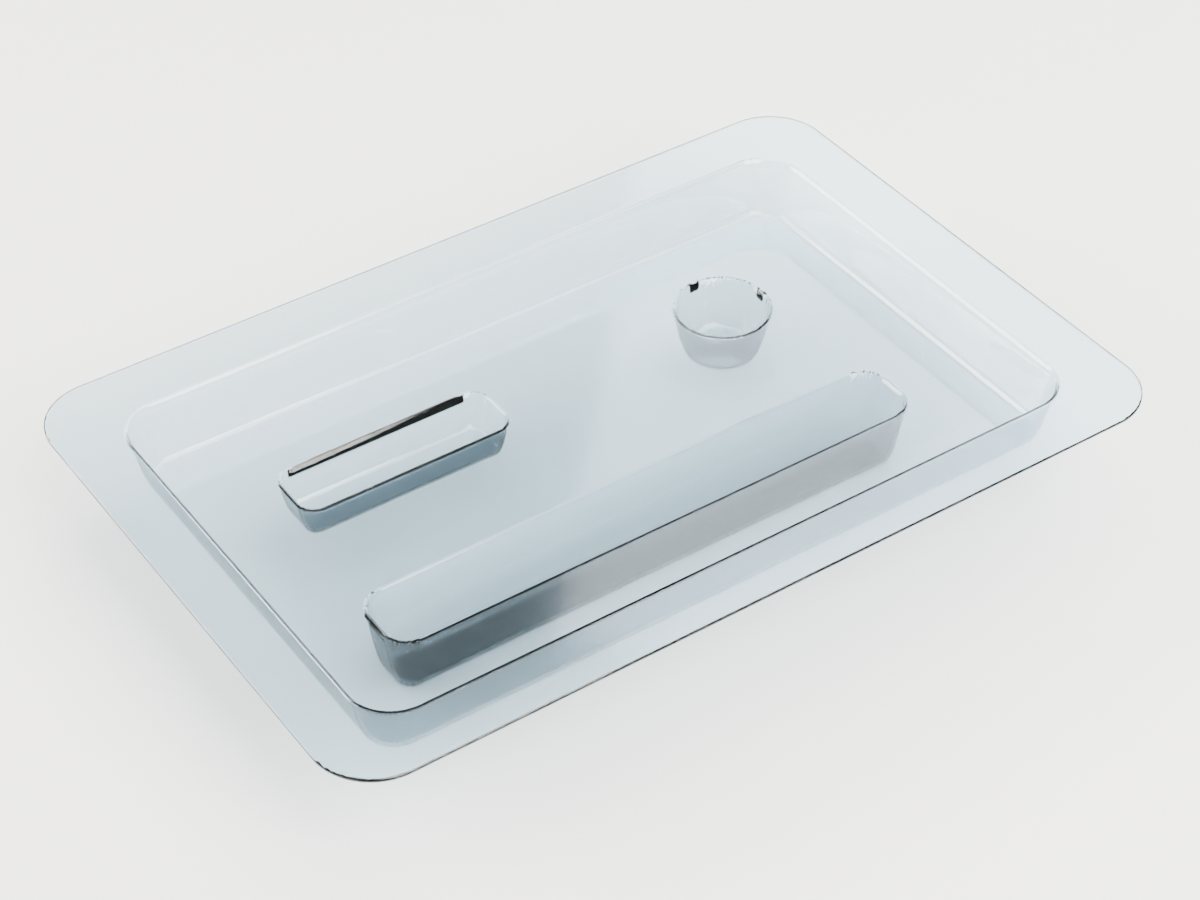
Medical device tray
Healthcare
PET · 0.75 mm · 240 × 160 mm · 35 mm deep
4 per index (2 × 2)
| Model | Parts per hour |
|---|
| Eco | 2,880 |
|---|
| Mid | 3,490 |
|---|
| Pro | 5,150 |
|---|
clear PET, stepped pockets
Bakery clamshell, hinged
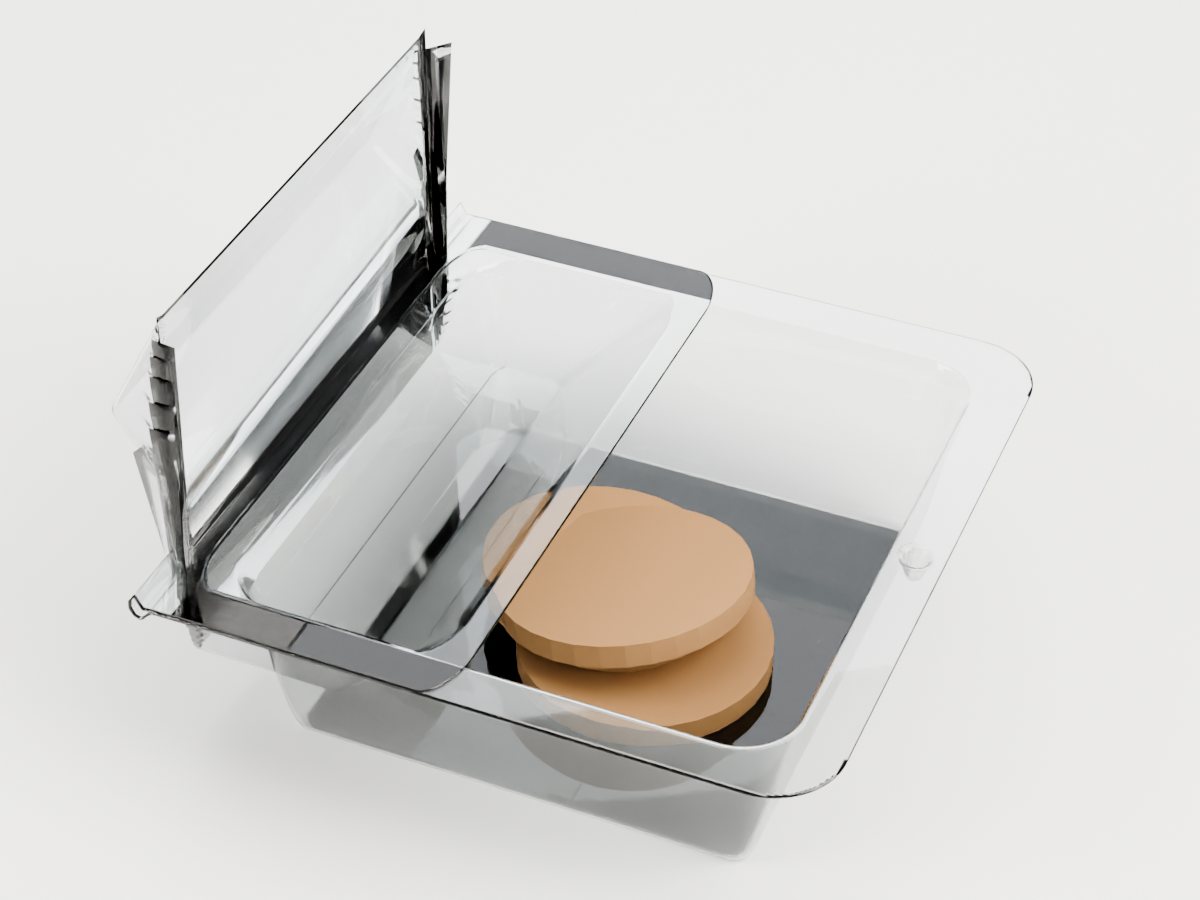
Bakery
PET · 0.35 mm · 180 × 340 mm · 50 mm deep
2 per index (1 × 2)
| Model | Parts per hour |
|---|
| Eco | 1,580 |
|---|
| Mid | 1,900 |
|---|
| Pro | 2,930 |
|---|
clear PET, base and lid in one
Electronics handling tray
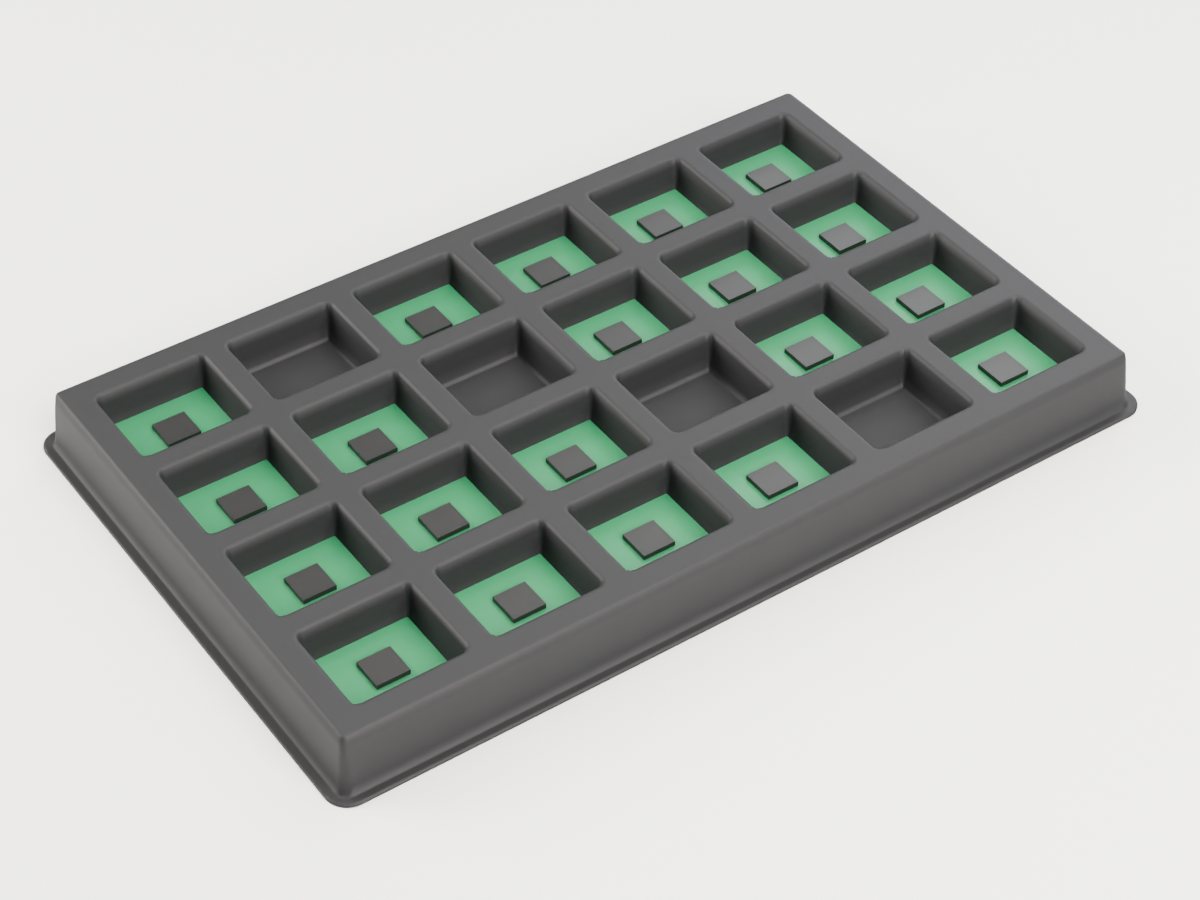
Electronics
HIPS · 1 mm · 320 × 200 mm · 22 mm deep
2 per index (1 × 2)
| Model | Parts per hour |
|---|
| Eco | 1,190 |
|---|
| Mid | 1,480 |
|---|
| Pro | 2,020 |
|---|
black conductive HIPS, 24 pockets
Drawer organiser insert
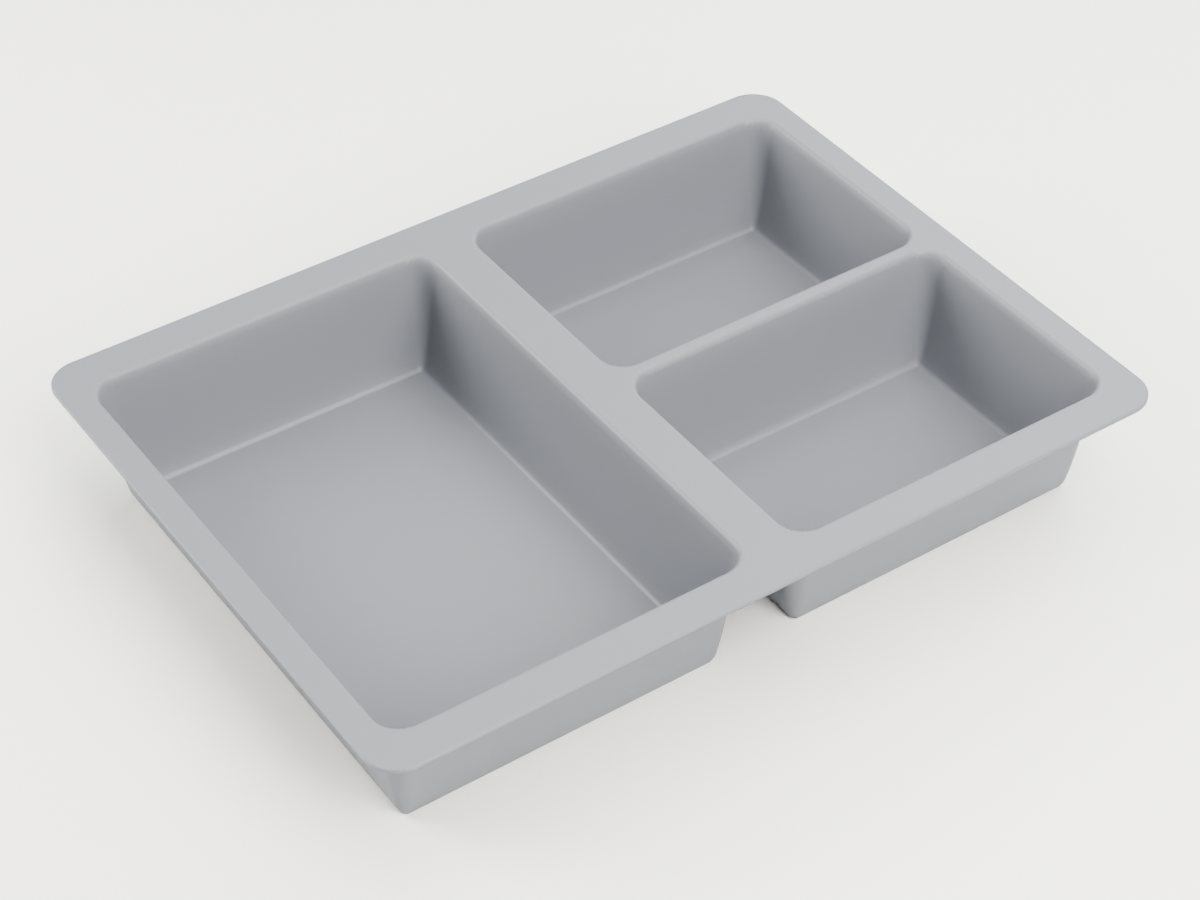
Home and furniture
ABS · 1.2 mm · 300 × 220 mm · 45 mm deep
2 per index (1 × 2)
| Model | Parts per hour |
|---|
| Eco | Sheet over 1.0 mm |
|---|
| Mid | 1,200 |
|---|
| Pro | 1,540 |
|---|
grey ABS, three compartments
Nursery plug tray
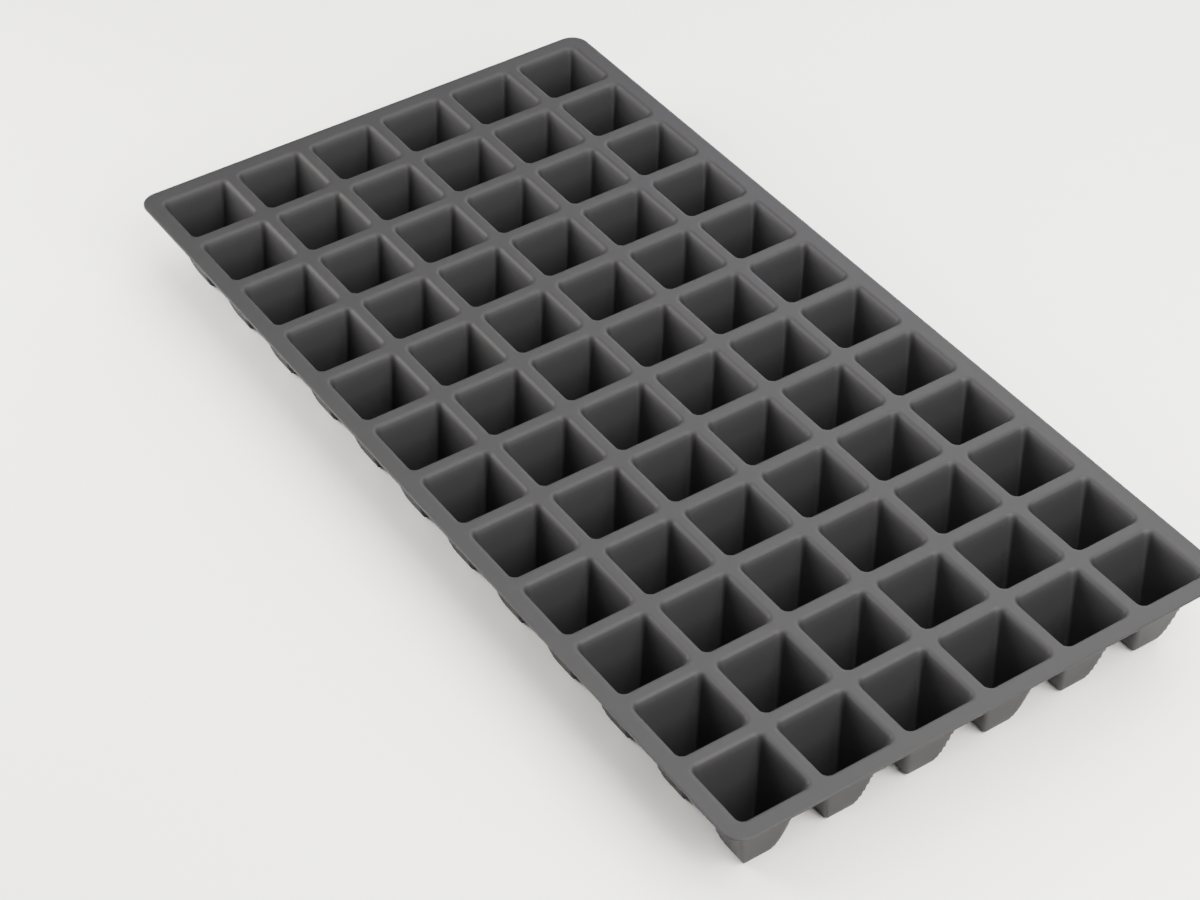
Horticulture
HIPS · 0.8 mm · 280 × 540 mm · 45 mm deep
1 per index (1 × 1)
| Model | Parts per hour |
|---|
| Eco | 660 |
|---|
| Mid | 810 |
|---|
| Pro | 1,150 |
|---|
black HIPS, 6 × 12 cells
Parts per hour, by application.
Parts per hour at full speed, log scale. A missing dot means the model cannot run that part.
How we worked these out
Simulated, not guessed. Each part runs through the physics model behind our live simulators: oven, sheet heating, forming, cooling and the trim press, cycle by cycle.
1. Nest the part. As many cavities as fit the 500 × 600 mm area, with a gap of 12 mm or 0.45 × depth, whichever is larger.
2. Heat to the right temperature. Heater setpoints are solved until the sheet reaches the material's ideal forming temperature, evenly across the web.
3. Cool long enough. Cooling time follows the material, gauge and depth, so parts hold shape after release.
4. Run it steady. Cycle rate is read once the machine is warm and every simulated shot passes the quality check.
Yearly figures in the data assume 2 shifts × 8 h × 300 days at 85% OEE. Rates are for sizing; a real rate is confirmed on your tool.
Your part is not on the list?
Get a quote
